lead forensics image

Viscous Product Pump for Relish & Chilli Jam at Tracklements

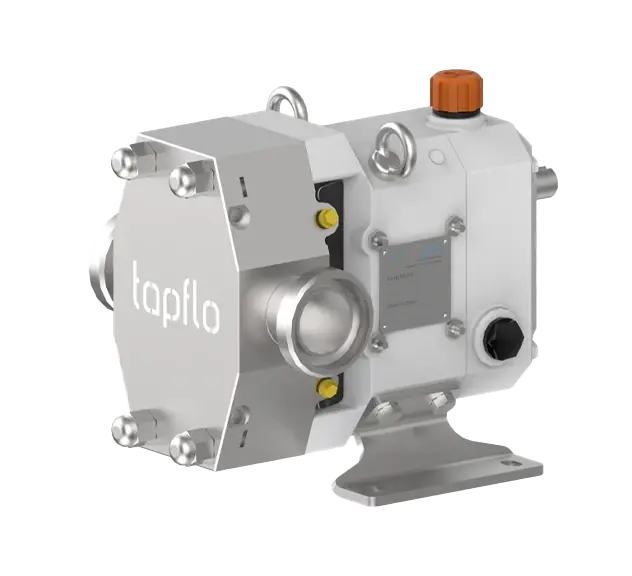
Tapflo UK supplied Tracklements with a LPX Hygienic Lobe Pump as the viscous product pump for its sticky fig relish, M&S hot products and chilli jam, replacing a sanitary lobe pump that had failed on site. The LPX easily transfers product up to 100 °C and a viscosity of between 1,000- 5,000 cPs. Tracklements has been pleased with the pump’s performance, benefiting from its reliable, efficient handling of high-viscosity products.

The Challenge

Tracklements, a manufacturer of relishes and jams, required a pump at its product facility in Wiltshire, UK.

When one of the site’s sanitary lobe pumps failed, Tracklements promptly contacted Tapflo UK for support. With the festive period fast approaching, they urgently needed a replacement to minimise disruption to production, particularly as the team was manufacturing hot products and chilli jam for retail giant M&S.

They needed the new viscous product pump to take over the same duty, connect directly to the site’s existing RJT pipework, and handle a product up to 100 °C with a viscosity of 1,000 to 5,000 cPs.

The duty:

  • Products: Sticky Fig Relish (including thick relish), hot products and chilli jam
  • Maximum temperature: 100 °C
  • Viscosity: 1,000 to 5,000 cPs
  • Flow rate: 3 m³/h
  • Transfer distance: Up to approximately 8 m through 1.5-inch pipework
  • Connections: RJT – to match the site

Solution

Tapflo UK assessed the duty on site with the Tracklements engineering team. Considering the application needs and the media being pumped, Tapflo recommended an LPX Hygienic Lobe Pump (LPX50). Benefits of this pump include:
  • Gentle, low-shear pumping of both low- and high-viscosity products
  • Large cavities between the lobes, allowing gentle pumping of liquids that contain solids
  • Gear oil isolated from the pumped product by the gear housing design, so there is no cross-contamination
  • Suitable for CIP (clean in place) and SIP (sterilise in place)
  • FDA-approved food contact materials
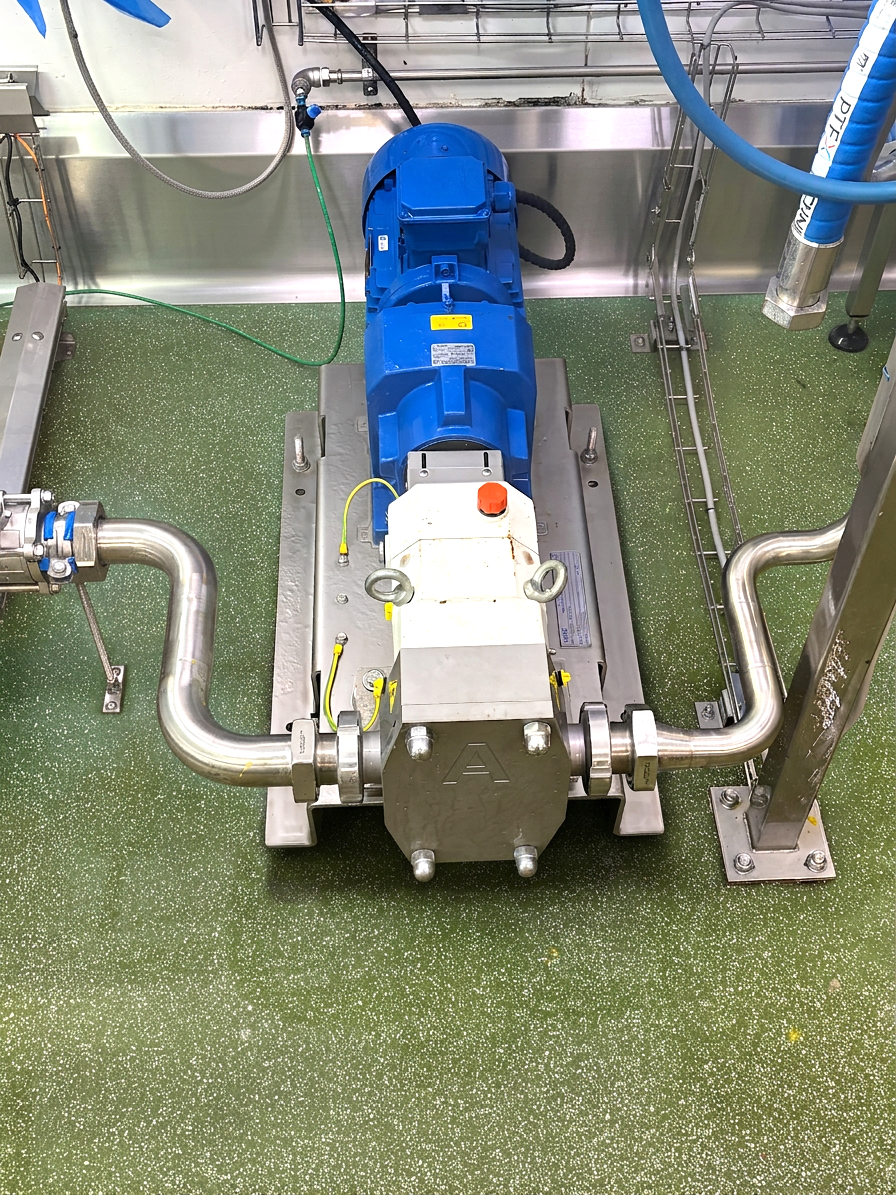
The pump was supplied with a frequency inverter, so Tracklements can set the pump speed to suit each product. Tapflo UK supported the site team in installing the inverter and is supplying a shroud to protect the pump from potential spills, mounted on pins welded to the existing baseplate to improve stability.
hygienic lobe pump from tapflo in a facility pumping viscous food products

The Results

The LPX replaced the failed pump for Tracklements’ viscous food products and is running smoothly and efficiently, pumping the required media at the correct temperature and transfer height.

Tracklements’ Engineering Manager rated Tapflo UK five stars in a Google review:

“Fantastic service, technical knowledge and communication from Stephen and Edward, I look forward to doing more business with Tapflo in the near future. Highly recommend.”

– Engineering Manager, Tracklements
For more on choosing pumps for thick food products, see the Tapflo UK guide to hygienic pumps for highly viscous products, or browse the full lobe pump range.

Written by

Adam Evans

| Design and Engineering Manager

Adam Evans, Process & Mechanical Engineering Manager at Tapflo Pumps UK, has over 10 years of expertise in the process industry. Adam’s wealth of experience and technical insights contribute to the development of innovative pump solutions and the continuous improvement of engineering processes.

FAQs

What pump is suitable for viscous food products like relish?

Can a lobe pump handle food products at 100°C?

Why fit a frequency inverter to a Lobe Pump?

Is the LPX Hygienic Lobe Pump suitable for CIP?

What pump is suitable for viscous food products like relish?

A hygienic positive displacement pump, such as a lobe pump, suits thick food products because it moves a fixed volume per rotation with low shear. Tapflo UK supplied Tracklements with an LPX Hygienic Lobe Pump to transfer relish and chilli jam at up to 100 °C and 1,000 to 5,000 cP.

Can a lobe pump handle food products at 100°C?

Yes. Tapflo UK’s Lobe Pumps are suited to temperatures up to 140 °C. At Tracklements, an LPX Hygienic Lobe Pump transfers relish and chilli jam at up to 100 °C.

Why fit a frequency inverter to a Lobe Pump?

A frequency inverter controls the motor speed, and with a lobe pump the flow rate follows the speed. The LPX Hygienic Lobe Pump Tapflo UK supplied to Tracklements has an inverter so the site can adjust the pump to suit each product.

Is the LPX Hygienic Lobe Pump suitable for CIP?

Yes. The Tapflo UK LPX Hygienic Lobe Pump is suited to CIP and SIP, uses FDA-approved food contact materials, and isolates its gear oil from the pumped product to prevent cross-contamination.

Latest Articles

a view of a filtration skid system in an industrial bakery facility
Case Study
|
2 min

Industrial Water Filtration System for a New Bakery Production Site

READ MORE
An up close photo of an ATEX Diaphragm Pump
Blog
|
4 min

AODD vs EODD: Air Operated vs Electric Diaphragm Pumps Explained

READ MORE
a water treatment facility from a birds eye view
Blog
|
5 min

Wastewater Pumps: Why Peristaltic Pumps Suit Sludge & Dosing Applications

READ MORE
peristaltic vs progressive cavity pump
Blog
|
5 min

Peristaltic Pump vs Progressive Cavity Pump: How to Choose

READ MORE