lead forensics image

Drum & Container Pumps

Electric and pneumatic options, designed to handle a variety of liquids from low-viscosity to highly viscous, aggressive, and flammable substances.
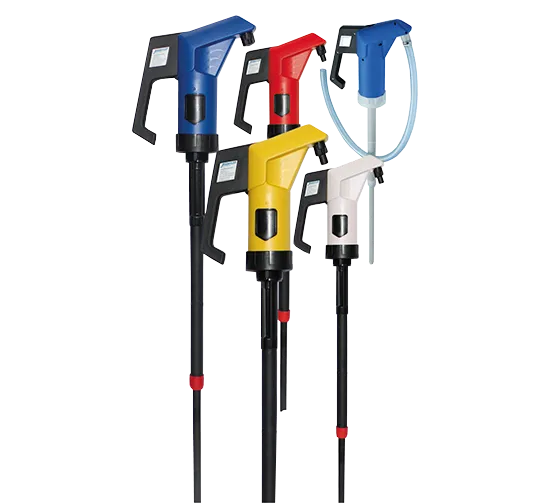
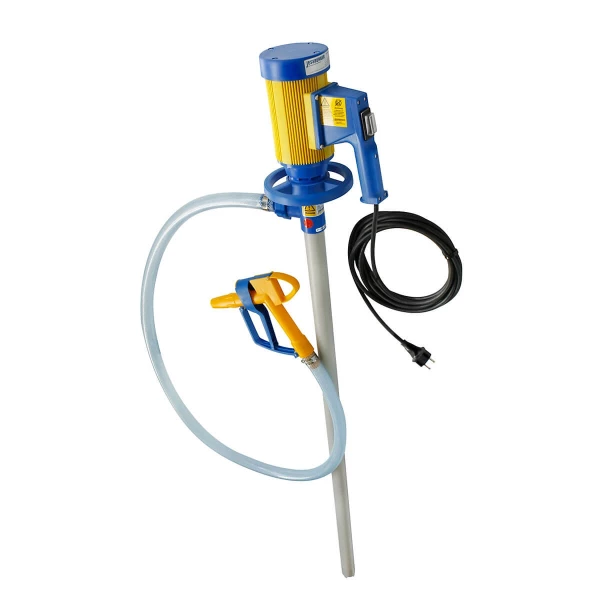
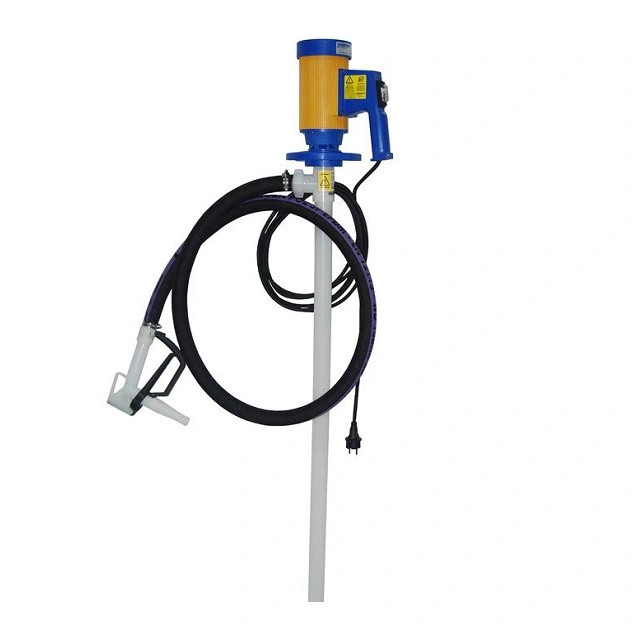
Tapflo Jessberger Drum Pumps
see more information
Tapflo Jessberger Drum Pumps

filter

Results 1-9 of 9
Results 1-9 of 9

Features & Advantages of Drum Pumps

  • Smooth, High-Performance – Effortless fluid transfer with flow rates of up to 200l/min in a compact pump
  • User-Friendly – Easy installation, safety features and overload protection with many models
  • Durable – Constructed from high-grade materials and robust impeller for continuous operation
  • Chemical Resistance – Ideal for chemical, fuels and mineral oil products with robust seals and corrosion resistant materials
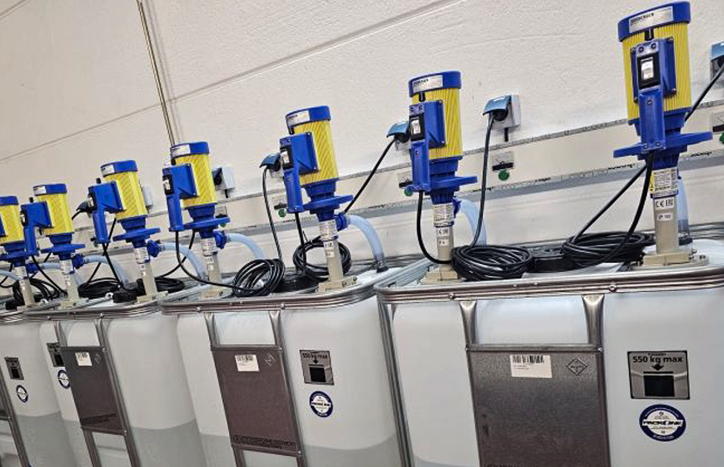
jessberger drum pumps situated on top of IBCs in a facility

Learn more about Drum Pumps

What is a Drum Pump?

What are the common industries and applications of Drum Pumps?

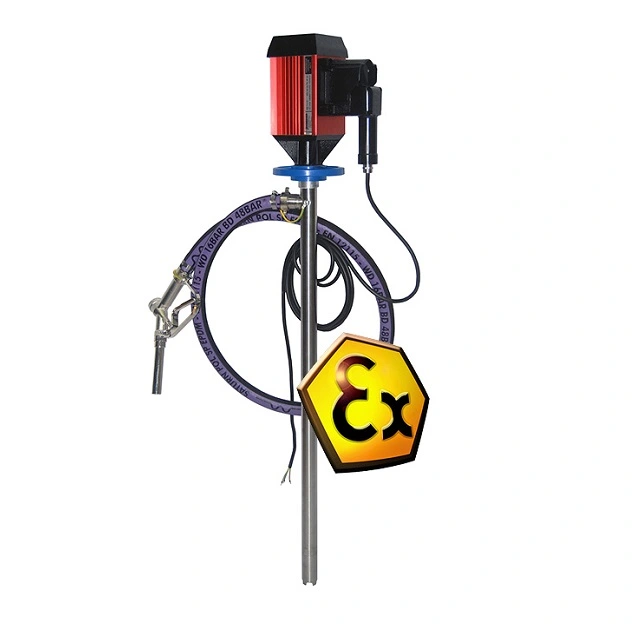
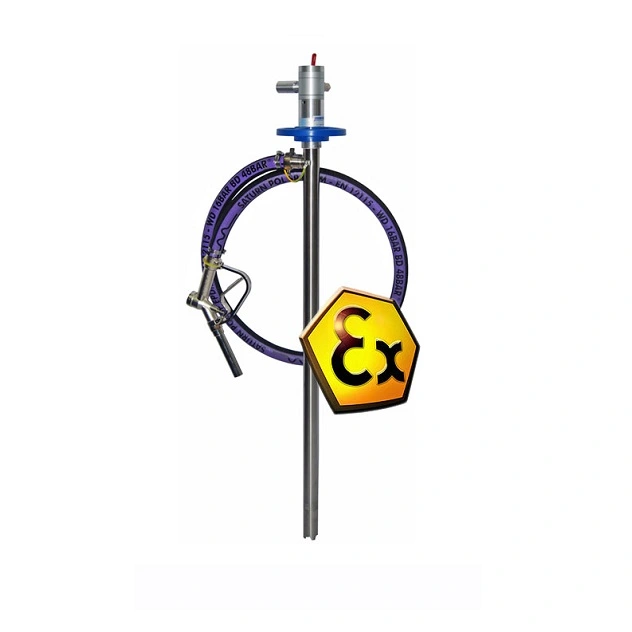
Are Drum Pumps suitable for ATEX environments?

What materials do Drum Pumps use?

What to consider when selecting a Drum Pump

What maintenance is required with a Drum Pump?

What is a Drum Pump?

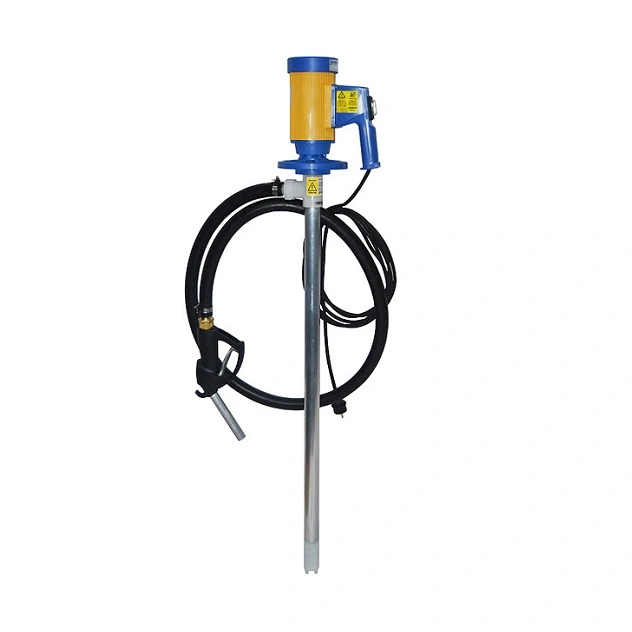
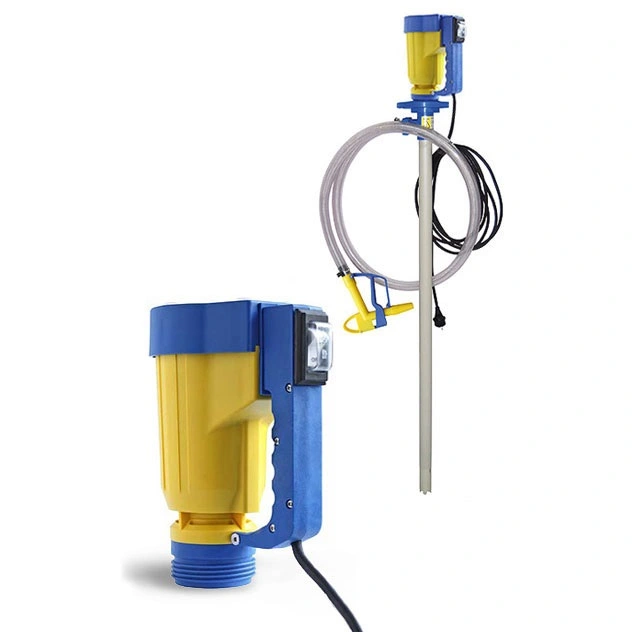
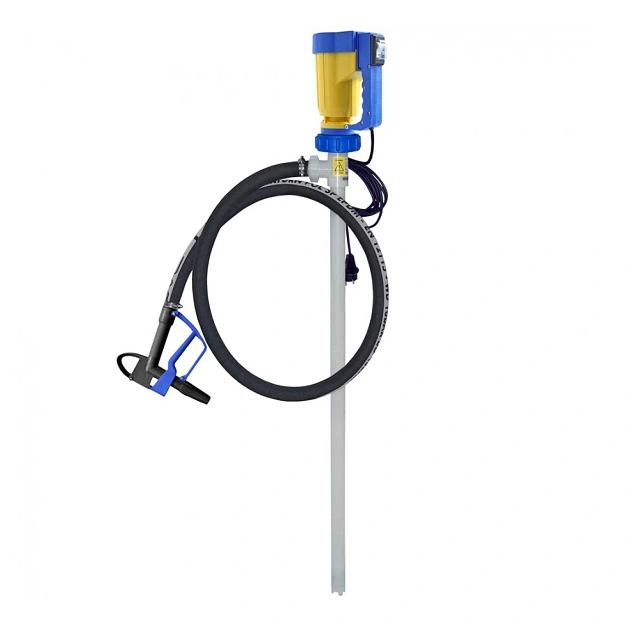
A Drum Pump is a type of Vertical Immersion pump designed for transferring liquids from drums or containers. They are available in electric, pneumatic and manual options and built to meet the needs of various industries, including chemicals, oils, and other industrial media.

What are the common industries and applications of Drum Pumps?

Drum Pumps are widely used across:


  • Chemical
  • Automotive
  • Pharmaceutical
  • Food & Beverage
  • Petrochemical industries


They are ideal for transferring both low-viscosity and medium-viscosity liquids such as acids, oils, fuels, solvents, and cleaning agents, as well as flammable and non-flammable media.

Are Drum Pumps suitable for ATEX environments?

Many Drum Pumps are ATEX certified; however, check the product description to confirm the specific model is suitable for ATEX environments.

What materials do Drum Pumps use?

Drum Pumps are made from several materials to suit different media:


  • Polypropylene: Ideal for acids, alkalis, and cleaning agents
  • PVDF: Suitable for aggressive chemicals like hydrochloric acid
  • Aluminium: Used for mineral oils, lubricants and fuels
  • Stainless Steel (1.4571): Best for flammable liquids, food products and applications requiring conductivity

What to consider when selecting a Drum Pump

When choosing a Drum Pump, you must consider a few factors such as:


  • Fluid Compatibility: Ensure the pump material is compatible with the media being pumped
  • Temperature Range: Select the appropriate material based on the fluid’s temperature (e.g., polypropylene for up to 50°C, PVDF for up to 90°C)
  • ATEX Considerations: When pumping flammable liquids, ensure the pump is compatible with ATEX guidance (Ex-Zone 0 or 1)
  • Accessories: Consider additional accessories such as hoses, nozzles, and flow meters to optimise efficiency and safety

What maintenance is required with a Drum Pump?

Drum Pumps require regular maintenance to ensure long-lasting performance. Key maintenance tasks include:


  • Checking the motor coupling, bearings, rotor, and pump tube components.
  • Checking wear parts such as the carbon or PTFE bearing, rotor, and shaft should be inspected periodically and replaced as needed.


Proper maintenance reduces downtime and extends the pump’s lifespan.