Tapflo’s Centrifugal Pumps, but with superior performance in flow range and pressure? Yes please!
Background
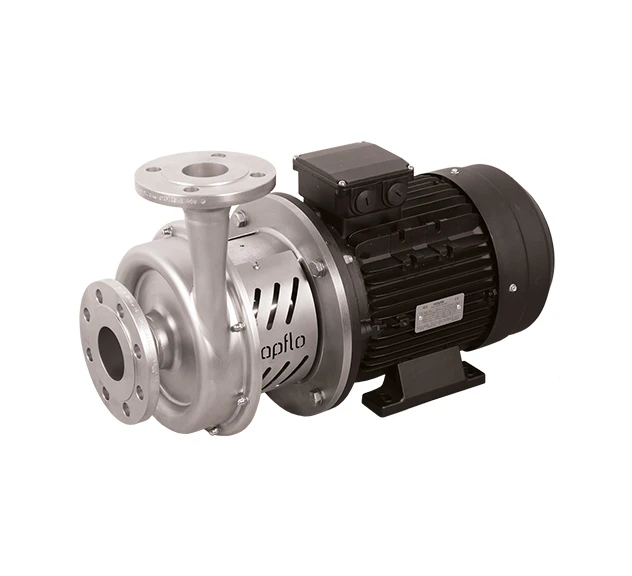
Building on Tapflo’s existing High Performance Centrifugal Pump range, the CTX offers sizes for an increased flow range and can reach higher pressures than our existing ranges. The CTX Pump range is available in hygienic and industrial executions which allows Tapflo to provide a wider variety of pump options to our customers for an assortment of applications. This allows the pump to be more flexible with quick and easy upgrade options available including the interchangeability of parts.
Industries that would benefit from the CTX range include chemical, pharmaceutical, food and beverage industries.
Range Overview
This new range offers a premium Centrifugal Pump that features high efficiency and a robust design with the option for a double mechanical seal that has no contact with the pumped liquid and is lubricated in a barrier fluid. This feature is ideal for ATEX regulations. Other benefits include easy cleaning and being competitively priced compared to similar pumps on the market.
“The CTX has better performance and efficiency than other similar pumps on the market, and at a low and extremely competitive price. Like all other Tapflo Pumps, we can deliver the CTX straight from our own factory and our stores worldwide, short delivery times is a part of our mission.” – Håkan Ekstrand, CCO (Chief Commercial Officer) at Tapflo Group.
“The CTX unit is something that Tapflo UK are very excited about. Tapflo Group have fulfilled their ambition of bringing a new and improved centrifugal pump to the global market that offers a cost effective solution with great reliability, minimal downtime and versatile design that can be used within many different sectors.” – Luke Simpson, Sales Manager at Tapflo UK.

